Precision Light Guide Molding: Ultra-Pure Optical Solutions
Discover how ENGELs innovative plasticizing technology elevates light guide quality and production.
Less Pellet Stock Means More Quality in Light Guide Production
Ever noticed how LEDs are transforming modern car designs? They’re becoming key differentiating elements in automotive lighting, bringing new geometric variations and creative possibilities. But with these innovations come fresh challenges for manufacturers of light guides.
ENGEL has developed an exciting new plasticizing process specifically for manufacturing high-quality light guides. The technology increases melt homogeneity and purity, giving lighting designers more freedom to create complex, elongated structures with superior luminous efficiency.
What Makes a Quality Light Guide?
A quality light guide needs to transmit light over long distances without losing intensity or altering color. This requires an exceptionally smooth surface throughout the entire transmission path to ensure total internal reflection. Light should only escape at specific points where prism-like structures are intentionally designed.
Injection molding is ideal for light guide production because it combines design freedom with cost efficiency - but the process demands:
- High-precision surface reproduction
- Exceptional material homogeneity
- Ultra-pure plastic melt
ENGEL AUSTRIA GmbH took on this challenge alongside several development partners. The result? An optimized injection molding process for polymethyl methacrylate (PMMA) that produces ultrahigh-purity light guides - perfect for even longer, more complex LED applications like outline lighting.
PMMA is a favorite material in automotive lighting, particularly for innovative cockpit lighting concepts. To ensure real-world relevance, the development team used demo light guide structures provided by Volvo Car Corporation. All trials were conducted using a family mold from Inevo (part of the INglass Group during the project).
Starve-Feeding: The Secret to Reducing Shear Load
The test production featured three light guides with different lengths and shapes produced in a single shot. The longest guide required gating at two points. They used Altuglas V825T LPL-grade PMMA to maximize light yield with these specific development goals:
- Surface roughness below 25 nm (greater roughness means blue light isn’t completely reflected, resulting in a yellowish tint)
- Zero contaminants (any contamination causes light scattering)
- No microcavities (which also scatter light)
The key innovation here is “starve-feeding” - a principle for which ENGEL developed specialized software. This technique deliberately reduces the amount of granules fed to the screw compared to conventional injection molding. The cylinder’s feed zone is only partially filled with granules, which are then compressed toward the screw tip where they completely fill the cylinder.
Think of it this way: less material in the cylinder means reduced torque and lower shear forces on the melt, which minimizes material degradation. To prevent oxidative degradation simultaneously, the team flushed the melt cylinder with nitrogen via the feed zone.
Plant Concept with Built-In Quality Testing
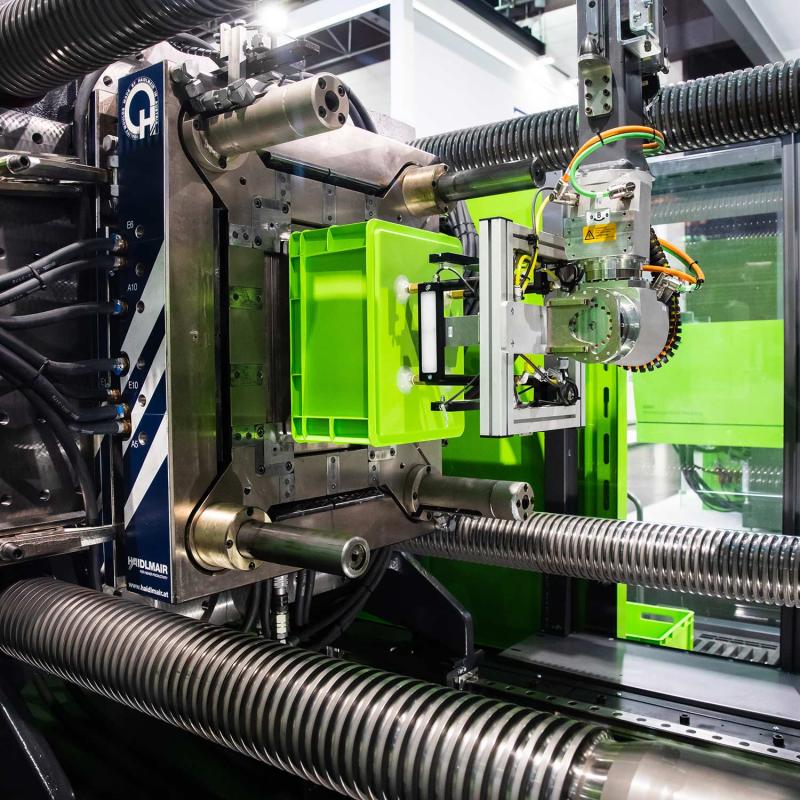
Tests were performed on an ENGEL e-motion 310/120 TL injection-molding machine featuring a screw and non-return valve specifically designed and coated for PMMA processing. This all-electric machine series offers both efficiency and high precision - crucial for demolding the very fine light-outcoupling structures on the parts.
The setup included quality-focused ancillary equipment:
- A Luxor EM-A 60 granules dryer
- A Minicolor dosing unit with dosing disk
- HRSflow’s FlexFlow system with electrically operated needle valves that could be individually actuated
To ensure consistent quality, the team integrated an inline testing system. After each shot, the smallest rod-shaped light guide (15 cm) was tested at a station with an LED light source. A Radiant Vision Systems device measured changes in correlated color temperature (CCT) - essentially how the human eye perceives light color.
Measuring Quality Through Color Temperature
CCT is an excellent quality indicator for light guides. The light color depends on the object temperature (with black radiator as reference) and the LED source characteristics. Temperatures below 3,000K appear as warm colors, while those above 3,000K appear cold.
Here’s the key insight: the less the CCT value deviates from the reference value (the LED source’s light color), the higher the quality of the light guide.
The trials clearly demonstrated starve-feeding’s benefits. Best results came when the melt cylinder was moderately filled (around 65%). Interestingly, reducing material feed too much actually decreased optical quality because longer metering times significantly increased melt shear loading.
Nitrogen purging provided additional benefits by displacing oxygen and preventing plastic melt oxidation.
Finding the Sweet Spot in Process Parameters
The team discovered several process parameters that influence light guide quality:
-
Screw speed: While 0.3 m/s circumferential speed was specified for the PMMA used, an even slower plasticizing rate significantly improved optical quality.
-
Injection speed: Higher speeds initially improved quality but eventually decreased it as pressure and shear loading increased too much.
-
Mold temperature: Higher temperatures improved surface reproduction, increasing CCT constancy.
-
Dust removal: Less dust in granules and melt reduced light scattering in the final product.
New Horizons in Lighting Technology
ENGEL’s newly developed plasticizing process opens exciting possibilities in lighting technology. The combination of starve feeding with optimized processing allows manufacturers to produce long, complex-shaped light guides with exceptional optical quality. The inline measurement system ensures consistent assessment and permanent quality control.
While all-electric injection molding machines (like the e-motion series used in development) are typically preferred for light guide production, this new plasticizing technology can be combined with various injection molding machines and drive technologies. ENGEL can integrate the associated ancillary systems into the plant concept at customer request, and the technology isn’t tied to specific ancillary system brands.
This innovation represents a significant step forward for automotive lighting designers looking to create more sophisticated, efficient LED applications with complex geometries and superior light transmission.